Intermittent Bonded Ribbon Production Line Available For Sale
A specified speed of 600 m/min gives this equipment considerable production capacity for optical-fiber applications. Before making purchasing plans, buyers should verify the actual speed, configuration, and operating conditions with the manufacturer.
Shanghai Weiye OFC supplies equipment designed specifically for producing rollable ribbons containing 12 or 16 fibers. The published product information covers capabilities, technical details, and supplied systems, helping U.S. buyers begin evaluating the equipment against their manufacturing needs.
Begin by examining the stated equipment configuration, then ask the supplier for pricing, installation requirements, and project-specific alternatives. This approach helps determine which equipment details apply to your particular manufacturing site and goals.
Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. provides its business address as 201 Minyi Road, Songjiang District, Shanghai. Use the product page for initial reference and verify current technical and commercial information directly with the company. A detailed quotation request can help advance your equipment evaluation.
Fiber Draw Tower
Fiber Coloring Machine
Fiber Draw Tower
Key Takeaways
- A speed of 600 m/min is listed, but buyers should verify the operating conditions with the manufacturer.
- The machinery is intended to manufacture rollable ribbons containing 12 or 16 fibers.
- The product listing describes machine capabilities, technical specifications, and supplied systems.
- Request details about pricing, installation requirements, and project-specific customization.
- The supplier provides a business address in Songjiang District, Shanghai.
Overview Of The Intermittent Bonded Ribbon Production Line
The manufacturer identifies this machinery as suitable for 12- and 16-fiber rollable IBR formats. The published specifications state a 600 m/min construction speed together with a fiber diameter of Ф245 μm ±10 μm. As these are manufacturer-listed values, confirm the actual production speed and relevant operating requirements directly with the supplier.
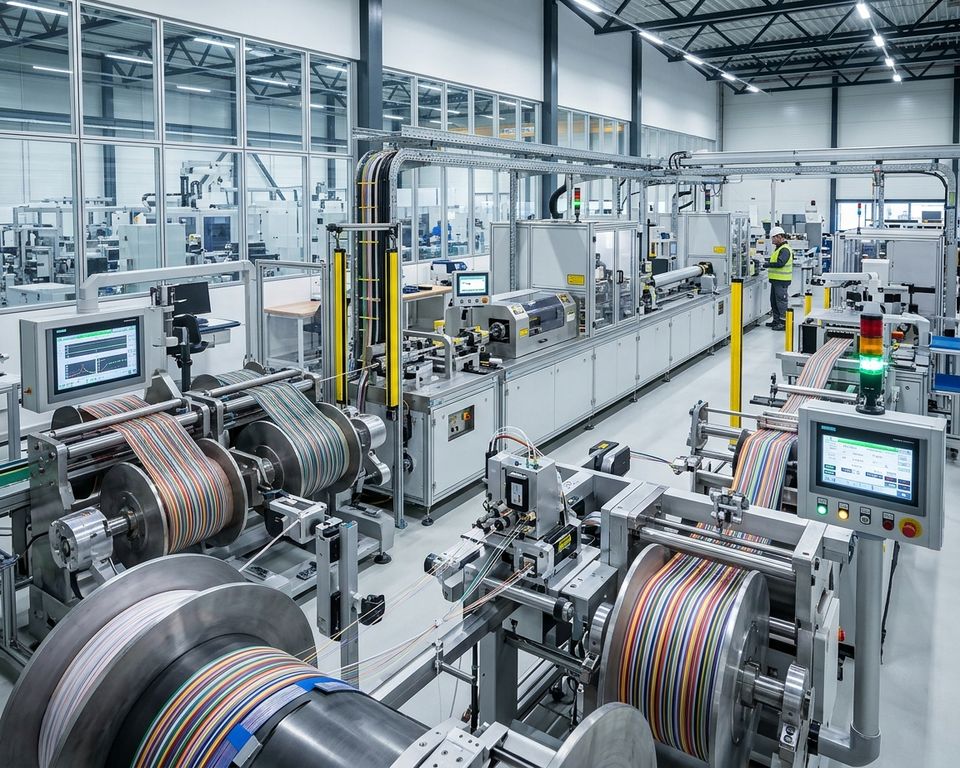 Intermittent Bonded Ribbon Production Line
Equipment Designed For Twelve- And Sixteen-Fiber Rollable Ribbon Production
The machine configuration accommodates two different fiber counts in rollable ribbon designs. This provides a useful reference when buyers compare machinery against their required ribbon format, fiber dimensions, and material-handling arrangements.
How Intermittent Adhesive Bonding Allows Flexible Fiber Configurations
According to examples in the patent, fibers are arranged in adjacent subunits with adhesive connections applied periodically. One illustrated spacing range extends from 10 mm to 1,000 mm. Unlike continuous bonding, this arrangement does not join the fibers along their entire length.
These intermittent adhesive connections allow the assembly to change from a relatively flat configuration into rolled, curled, or folded forms. The specified spacing illustrates the patented design concept rather than confirmed production-machine settings.
- Machine details: 12 or 16 fibers, a stated speed of 600 m/min, and a diameter of Ф245 μm ±10 μm.
- Patent example: Adhesive-bond intervals ranging from 10 mm to 1,000 mm.
- Design benefit: Adaptable handling when the ribbon takes different shapes.
Uses In Optical Fiber Cable Manufacturing
Flexible ribbon arrangements can help cable designers balance access for splicing with compact cable packaging. The patented design keeps fibers arranged in order while permitting sections between bonded points to shift as the cable is assembled.
High Fiber Density And Compact Cable Designs
An optical fiber ribbon may remain flat during mass fusion splicing and subsequently fold or roll for installation in a smaller cable. Potential advantages described in the patent include smaller cable constructions and an increased ratio of fiber area to overall cable cross-sectional area. The results achieved in practice depend on the complete cable construction and its intended use.
Organizing Fiber Ribbons To Support Efficient Fusion Splicing
This design supports orderly fiber handling during splicing while providing flexibility for subunit movement in the assembly process. The manufacturer’s material-handling specifications identify payoff reel capacities of 25.2 km and 50.4 km of fiber. These reel capacities can be compared with the facility’s cable-manufacturing needs and material-handling setup.
| Design characteristic | Potential use | Consideration for buyers |
|---|---|---|
| Flat fiber configuration | Fusion splicing of multiple fibers | Verify the needs of your splicing process |
| Folded or rolled format | Space-efficient cable packaging | Review the overall cable construction |
| 25.2 km and 50.4 km capacity payoff reels | Material-handling preparation | Match the reel capacity to production operations |
Production Line Specifications And Performance
Compare the equipment’s published performance figures with your manufacturing requirements before requesting a quotation. Installation preparations should also account for suitable reels and the utilities available at the production site.
Production Speed, Fiber Diameter, And Attenuation
According to the specifications, the construction speed reaches 600 m/min. The specified fiber diameter is Ф245 μm ±10 μm, while additional attenuation is stated as ≤0.01 dB/km at 1550 nm. Confirm the measurement conditions and expected performance directly with the manufacturer.
Compatibility With Payoff And Take-Up Reels
The payoff system accommodates two reel dimensions, and the maximum weight of a full reel is 10 kg. The take-up assembly supports a T-type reel as well as a fiber-optic reel. Check whether the preferred reel format suits your existing handling equipment and procedures.
Facility Utilities And Operating Environment
The machine requires a three-phase, five-wire electrical supply rated at 380 V ±10%. The equipment should operate in an enclosed, clean, dry, draft-free area maintained at 15 to 25°C and a maximum relative humidity of 85%. Nitrogen must be supplied at 7 bar with 99.99% purity, together with compressed air at 6 bar. Verify the required utility connections before installation begins.
| Technical specification | Published requirement | Installation planning note |
|---|---|---|
| Payoff reels | Payoff dimensions of Ф236 × Ф25.4 × 108 mm or Ф267 × Ф25.4 × 180 mm; full reel ≤10 kg | Verify reel dimensions and weight |
| Reel used for take-up | T-type reel: Φ410 × Φ50.8 × 391 mm, alternatively a fiber-optic reel | Confirm compatibility with your selected format |
| Power and environment | 380 V ±10%; 15 to 25°C; relative humidity ≤85% | Provide a clean, dry area without drafts |
| Gas utility supply | Nitrogen: 7 bar, 99.99% purity; air: 6 bar | Check available gas capacity before equipment setup |
Fiber Payoff And Gathering Equipment
The payoff and gathering assemblies direct optical fibers into the ribbon-forming area. The associated controls help maintain a steady supply of fiber while reducing handling risks.
Sixteen-Spool Payoff With Tension Control
The payoff assembly holds 16 spools and provides traversing along with separately adjustable tension settings. The permitted weight for an individual spool is up to 10 kg. The technical details list 0.4 to 2 N tension with ±0.02 N accuracy, together with a 550 W motor. Another overview gives a range of 40 to 150 g and accuracy of ±2 g, so buyers should confirm which specification applies to their configuration.
Fiber Guidance, Break Detection, And Static Control
U-groove guides, multi-groove gathering rollers, and anti-jump components channel fibers into the forming section. Operators receive alerts about fiber problems through break detection and alarm functions. Safe handling is supported by protective guards and a pneumatic clamping mechanism. At the fiber exit, a rod-style electrostatic dust collector is installed, while anti-static equipment helps manage dust along the gathering route.
| Equipment component | Listed detail | Intended function |
|---|---|---|
| Payoff | 16 spools with a maximum of 10 kg each | Feeds optical fibers with traversing movement |
| Tension and motor | 0.4 to 2 N with ±0.02 N accuracy; 550 W | Supports regulated payoff of fibers |
| Guidance and safety | Grooved rollers, alarms, guards, and pneumatic clamping | Guides fiber movement and assists material handling |
| Static control | Rod-type dust collector and anti-static equipment | Supports dust control along the fiber path |
Intermittent Adhesive Dispensing And Precision Molding
Operators can adjust adhesive positioning and mold alignment through the forming platform. Available adjustments help configure the process for each required ribbon format.
Adjustable IBR Mold Platform For Ribbon Formation
Ribbon formation uses three mold assemblies, each capable of holding up to five Nordson EFD jet valves. Operators can position the mold within 0 to 15 mm and adjust its base temperature from 20°C to 60°C. Grouped precision dispensing valves are installed on slide tables so operators can refine their alignment and place adhesive dots carefully.
Configurable Nozzle Arrangements For Twelve- And Sixteen-Fiber Ribbons
For 12-fiber ribbons, the specified arrangement consists of 5+5+1 valves. The 16-fiber format is produced using a 5+5+5 valve layout. Operators can adjust adhesive-dot spacing and the number of dots through the interface to match the selected optical fiber ribbon design. The process calls for a specialized adhesive suitable for both coating and curing.
| Setting | Format With 12 Fibers | 16-Fiber Format |
|---|---|---|
| Valve arrangement | Valve arrangement of 5+5+1 | 5+5+5 valve configuration |
| Mold positioning range | 0 to 15 mm adjustment | Adjustment range of 0 to 15 mm |
| Temperature of the mold base | Temperature range of 20°C to 60°C | 20°C to 60°C operating range |
UV-LED Curing For Bonded Fiber Ribbons
Adhesive across the fiber assembly is cured through a sequence of UV exposure stages. Prospective buyers can assess the oven configuration and listed operating specifications to determine whether the equipment suits their production process.
Pre-Curing And Main Curing Stages
Pre-curing is handled by three specialized 800 W LED-UV ovens. Fibers from each mold group pass through their respective pre-curing unit before entering the principal 6 kW post-curing oven. Adjustable shutters reduce potential UV leakage and nitrogen loss. Published specifications identify a dominant wavelength of 395 nm ±3 nm, a curing degree of at least 85%, and post-curing power of at least 2.5 kW.
Managing Nitrogen Supply And Curing Performance
Operators can manually regulate nitrogen pressure and flow. The system additionally switches nitrogen on when starting and off when shutting down. At production speed under continuous stable conditions, the specified lamp-array power consumption is no more than 80% of total power. The figures are useful for initial equipment assessment, but buyers should confirm the conditions under which they were measured. Ask whether different adhesives or materials require adjustments to the settings.
Visual Monitoring, Capstan, And Take-Up
As fibers travel through the equipment, visual monitoring and steady winding support the maintenance of material quality. Buyers can use the listed specifications to assess whether the machine meets the demands of their cable manufacturing process.
Online Inspection Of Fiber Color Sequence And Adhesive Dots
A microscope and camera provide enlarged images in real time. The display allows operators to check the sequence of fiber colors and confirm adhesive resin dots at each dispensing position. This inspection helps identify ribbon problems before the material enters the winding stage.
Servo-Driven Traction And Precision Take-Up
A 1 kW AC servo motor powers the capstan’s Φ190 mm traction wheel. Metering accuracy is specified as better than 1‰. Operators can set tension between 50 and 500 g while maintaining an accuracy of ±5 g. These operating parameters help maintain careful fiber-ribbon handling as the material advances through the line.
The specified take-up speed is 600 m/min, and the maximum spool weight is 30 kg. The servo-driven take-up and traversing assemblies support uniform positioning during winding. Cable pitch can be adjusted continuously between 1 and 6 mm. Position detection and direction changes are supported by a photoelectric sensor. Check the intended cable requirements and actual operating conditions with the manufacturer.
Production Monitoring And Electrical Control Systems
Clear control functions help production staff manage settings, monitor system conditions, and prepare smooth stopping procedures. The supplier identifies Siemens control equipment and Schneider Electric switchgear as components of the production line.
PLC And Touchscreen Operation
Siemens S7-1200 and S7-1500 PLCs manage the ribbon manufacturing system through a 10.4-inch Siemens touchscreen. Low-voltage switchgear is supplied by Schneider Electric. Operators may control the entire line with interlocked units or run individual sections independently.
Settings, Alarms, And Length-Based Stops
The touchscreen allows adjustment of process parameters, curing-oven activation, wire-feed settings, and alarm information. Additional displays provide lamp runtime, real-time current readings, curing-oven temperature, and total machine operating hours. A meter-counter correction function helps synchronize displayed length measurements with actual material movement.
Operators can program a target production length that triggers deceleration or shutdown. This provides a practical way to control the end of a cable production run. Ask the manufacturer to confirm control capabilities and setup requirements before placing an order.
| Control feature | Published specification | Practical function |
|---|---|---|
| PLC and display | Siemens S7-1200 and S7-1500 PLCs with a 10.4-inch touchscreen | Configure settings and examine production data |
| Electrical components | Low-voltage switchgear from Schneider Electric | Provides support for system control |
| Equipment monitoring and shutdown control | Lamp, oven, runtime, and meter information with preset length | Monitor production and stop or decelerate the equipment |
Ribbon Quality, Material Selection, And Process Compatibility
The selected adhesive influences coating uniformity and the quality of the finished ribbon. The manufacturer calls for a specialized adhesive intended for the machine’s coating and curing process instead of an ordinary multipurpose product.
Dedicated Adhesive For Bonding And Curing
The pressure-fed adhesive system provides independent valve switches so each supply path can be opened or closed as required. Precision pressure-regulating valves help maintain controlled adhesive delivery at each dispensing location. The specified air pressure is adjustable, with a required minimum of 0.5 MPa.
Black adhesive supply tubing helps protect the material from reactions caused by UV exposure during operation and curing. Preventing unintended exposure matters because adhesive behavior could be affected before the material reaches the fiber surface.
Before selecting materials for a secondary coating line, verify adhesive compatibility, production settings, and required surface-quality standards with the supplier. Ask how the recommended adhesive performs under your intended application conditions and expected production length. Detailed manufacturing guidance can support consistent quality throughout setup and the completed run.
Equipment Installation Needs And Supplied Documentation
Ensure the workspace and utility supplies are ready before scheduling the machine’s installation. The manufacturer’s stated requirements help buyers prepare their facilities and maintain stable operation of the optical fiber equipment.
Facility Conditions And Buyer-Supplied Connections
The machine should be positioned inside a draft-free, enclosed workspace that is clean and dry. Keep the operating area between 15 and 25°C, with humidity at or below 85%. Provide nitrogen at 7 bar and 99.99% purity, along with compressed air at 6 bar.
Connection cables and cable trays are excluded from the supplied equipment. The purchaser is responsible for supplying the main incoming power cable. Before installation, check cable routing and utility capacity, particularly when the machine will be located near secondary coating operations.
Operating Manuals, Drawings, And Maintenance Information
The supplier includes documentation supporting machine installation, operation, and servicing. Review these records before startup to help staff plan work activities and identify necessary supplies.
- Instruction manuals, operating guides, and a general layout drawing
- Electrical schematics, wiring diagrams, and drawings for installation and maintenance
- Purchased-component instructions and a wear-parts list to support service preparation
These documents help maintenance and production teams prepare for initial startup and regular equipment care.
Selecting A Ribbon Production Line That Matches Your Manufacturing Requirements
Begin by identifying the ribbon formats you intend to manufacture and sell. The machinery supports 12F and 16F formats and has a stated construction speed of 600 m/min. Assess the stated capabilities against your planned range of products, throughput requirements, and projected cable orders.
Verify take-up reel compatibility before placing an equipment order. The standard IBR reel has dimensions of Φ410 × Φ50.8 × 390 × Φ310 mm, supports up to 30 kg, and provides cable pitch adjustment from 1 to 6 mm. Check that these specifications suit your production facility and material-handling operations.
The compatibility of payoff spools should be reviewed as well. The listed choices include internationally standardized spools with capacities of 25.2 km, 50.4 km, and 63 km. Request precise reel measurements before selecting materials or determining production run lengths.
Evaluate utilities, adhesive requirements, and operator-monitoring capabilities alongside production speed. For cable manufacturing, determine whether the configuration suits fiber cable, loose tube, or another planned application. Before ordering, review equipment configuration and startup requirements directly with Shanghai Weiye. Checking equipment suitability in advance can reduce the likelihood of costly changes after purchase.
| Production planning consideration | Listed detail | Required buyer verification |
|---|---|---|
| Formats and speed | 12F, 16F; specified speed of 600 m/min | Compare with target production and product mix |
| Take-up | 30 kg maximum capacity; adjustable pitch from 1 to 6 mm | Check reel compatibility and facility requirements |
| Fiber payoff reel options | Capacities of 25.2 km, 50.4 km, and 63 km | Verify exact spool dimensions |
Request A Quote For The Intermittent Bonded Ribbon Production Line
U.S. buyers can evaluate a system offering 12F and 16F formats, a specified construction rate of 600 m/min, and specialized optical fiber ribbon-forming equipment. Use these specifications to determine whether the machine is appropriate for your intended cable application.
A pricing inquiry should include your chosen format, projected production quantity, reel requirements, and facility utility details. Also describe the fiber type and handling requirements so Shanghai Weiye can evaluate the proposed configuration.
Confirm the suitability of the adhesive, the LED wavelength specification of 395 nm ±3 nm, and expected curing results before purchasing. Ask the supplier how these parameters relate to the chosen materials and required surface quality.
Consult the product page for the published equipment description. Verify the final configuration, shipment details, and installation commissioning with Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. The supplier provides its address as 201 Minyi Road, Songjiang District, Shanghai. You can call 021-60701630 to review your project needs with the supplier. A detailed quotation inquiry helps define the next steps in purchasing.